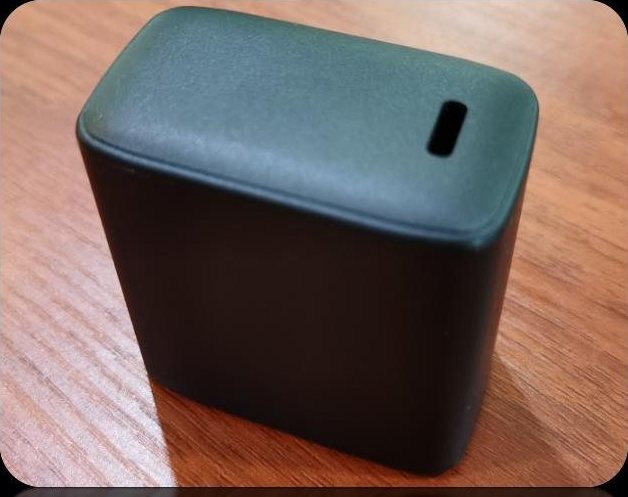
Zero-draft, slide-free molding
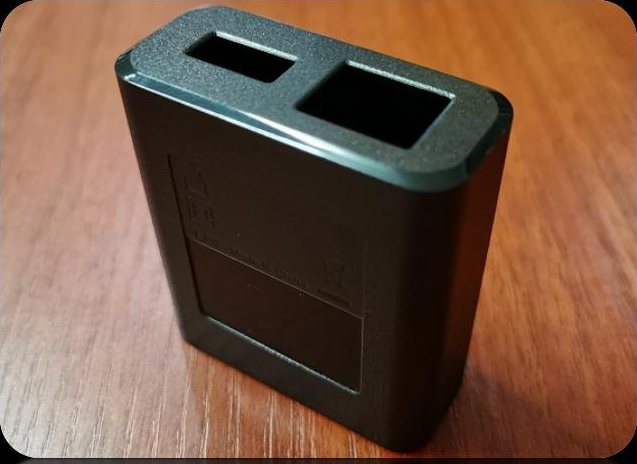
Straight-wall charger housings molded without slides: 163 mm tall, VDI 30 texture, no drag marks on the side walls.
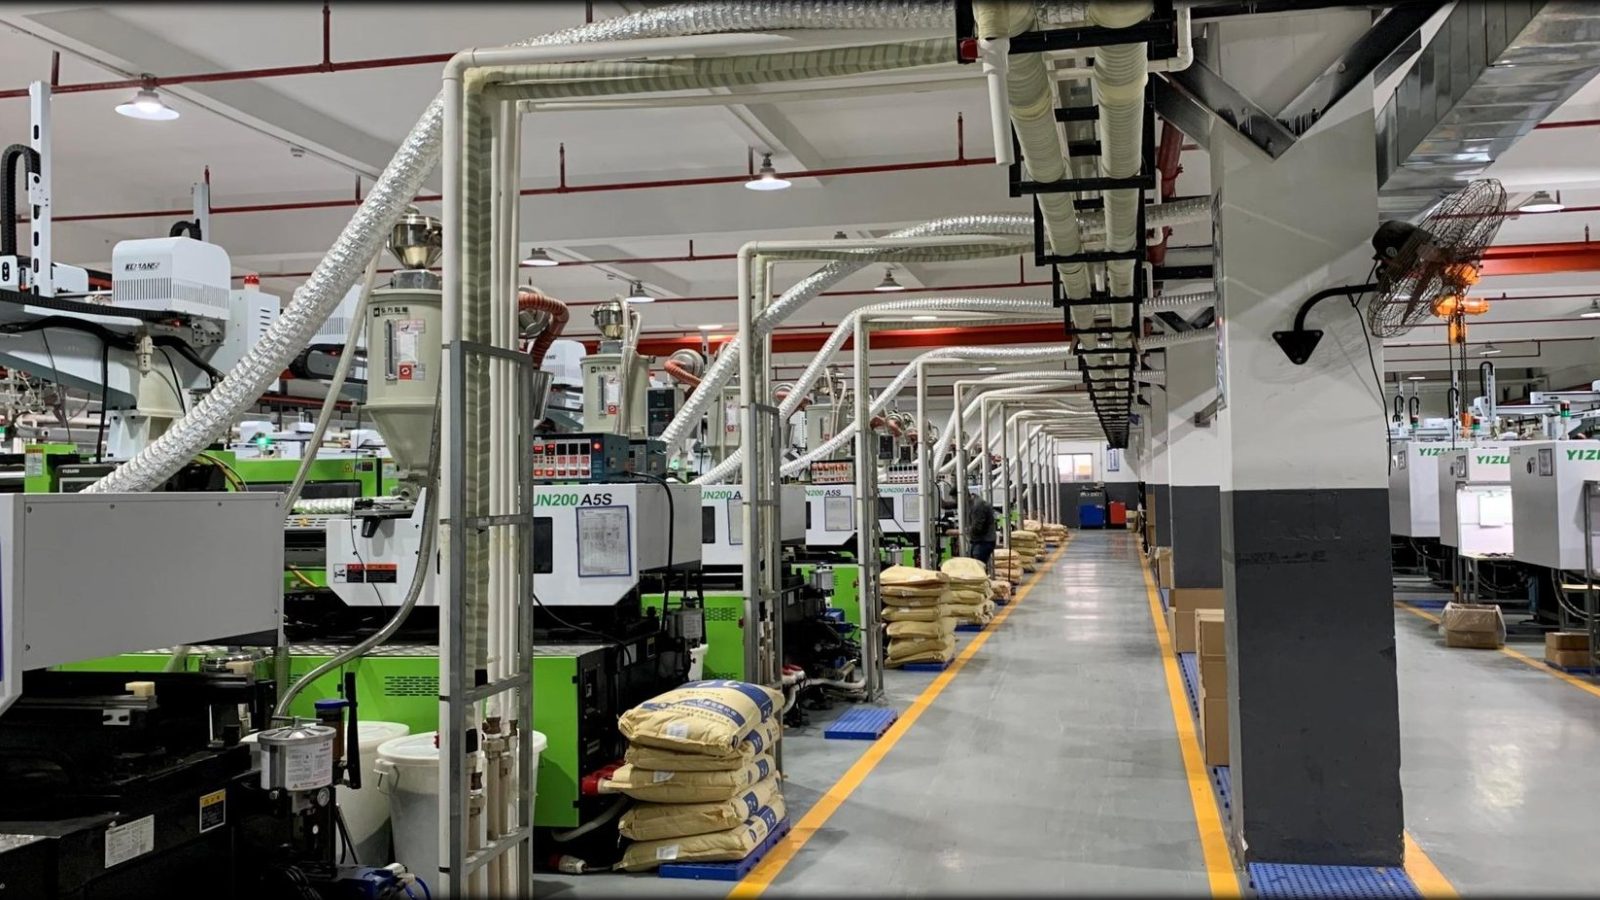
Mold making · Injection molding · Automation
We design and build the tool, then mold, automate and inspect the housing in one plant in Dongguan, Guangdong: 71 machines, 25 to 35 new molds a month, ISO 9001 and ISO 14001.
Product range
Each range below is produced on our own molds and molding machines. Open a range to see molded examples, housing construction and surface options.
 01
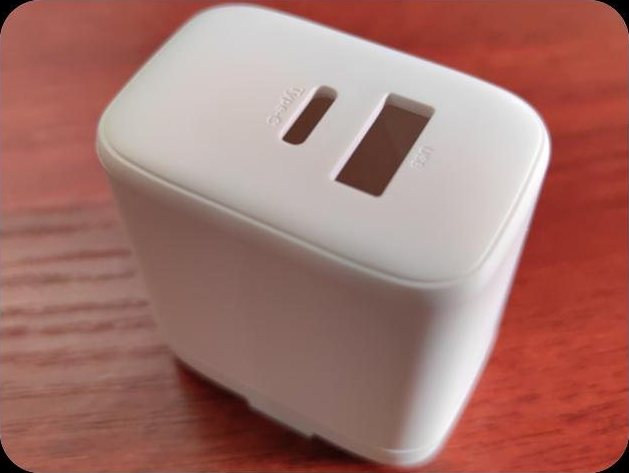
Wall Charger Housings
Compact charger bodies with fixed or folding pins. Straight side walls, fine textures and parting lines that stay…
 02
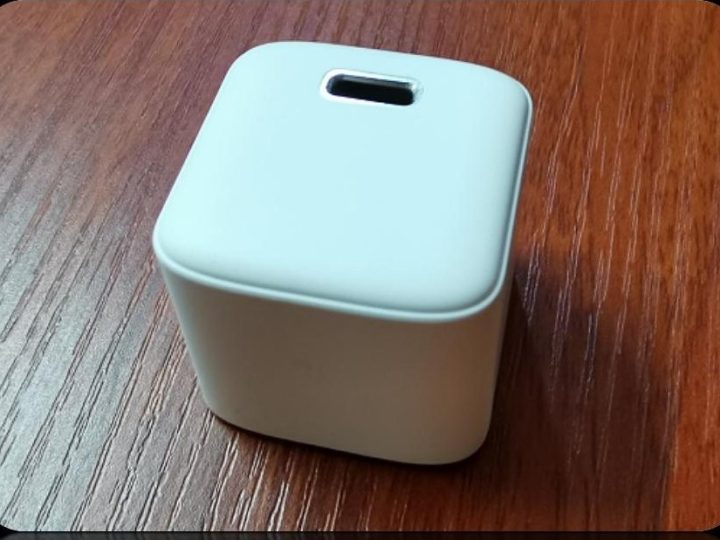
PD & Fast-Charge Housings
Multi-port fast-charge bodies with tight port tolerances, high-gloss faces and thin, straight walls that still pass drop and…
 03
Desktop Adapter Enclosures
Power brick enclosures molded in two halves, with vented panels, indicator windows, label recesses and internal screw bosses…
 04
Network Device Housings
Router, ONT and gateway housings with snap-fit covers, port cut-outs, wall-mount slots and internal ribs that keep the…
 05
Socket & Power Strip Components
Socket chassis, safety shutters, terminal blocks and end caps for wall outlets and power strips, molded in flame-retardant…
 06
Energy Storage Housings
Opaque and translucent housings for portable power banks, storage cells and battery tubes, including light-diffusing walls and perforated…
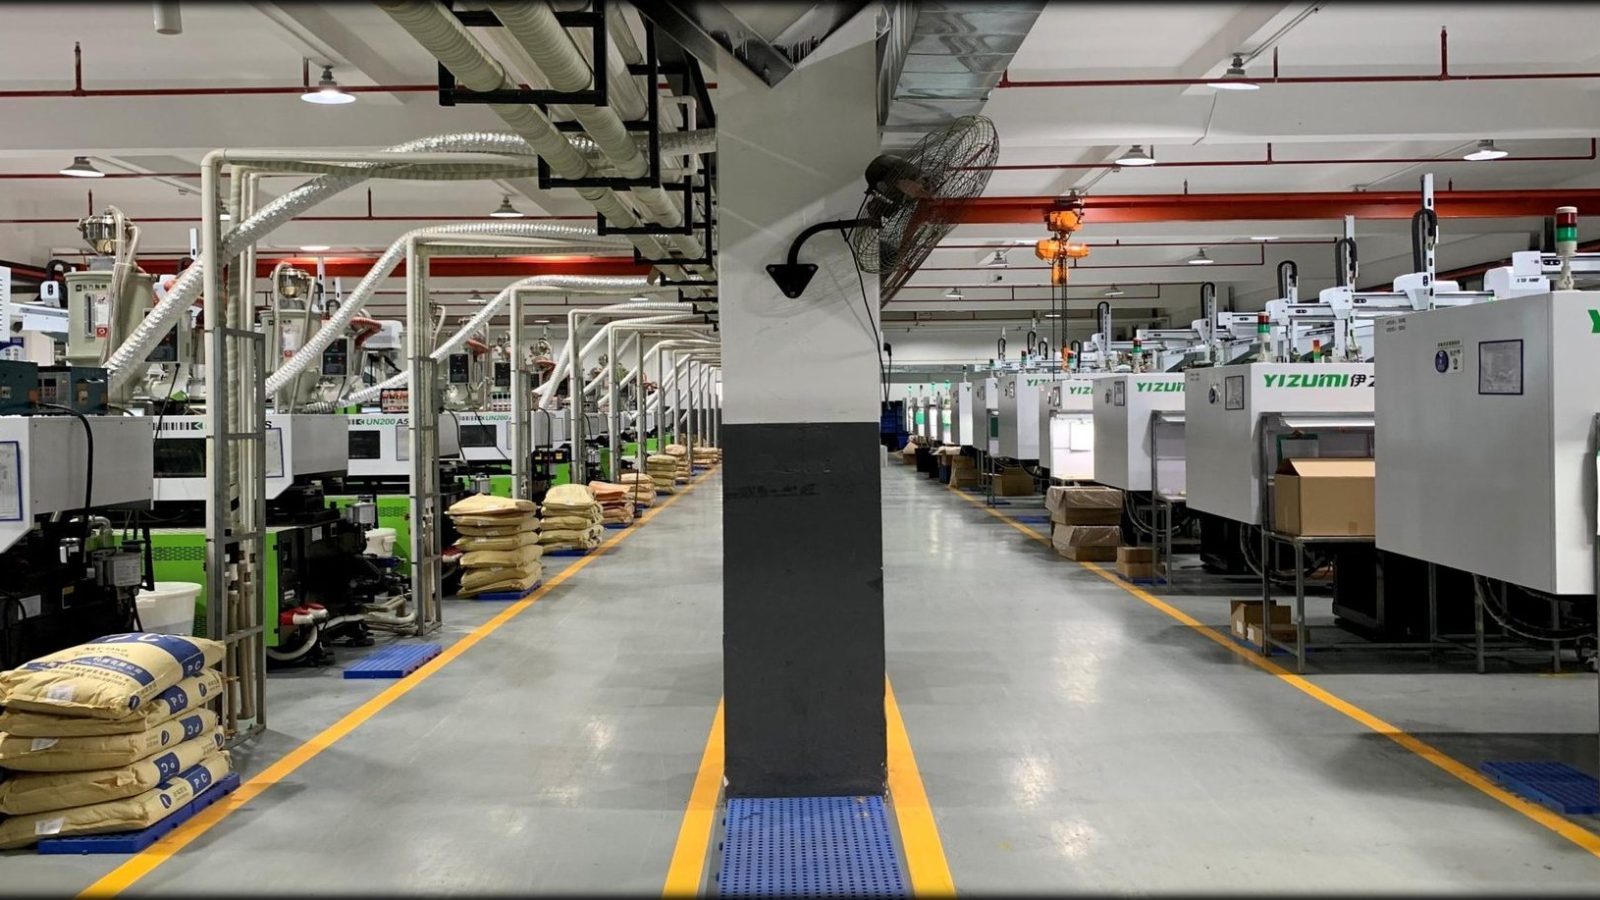
One plant, one owner for the tool and the part
Your project starts at DFM and ends with packed parts. Because the tool shop, the molding floor and the automation team sit in the same building, a mold change, a gate adjustment or a new insert machine is measured in hours rather than weeks.
Engineering
Straight walls, fine texture and invisible parting lines are where most housing projects stall. These are the methods our engineering team has already production-proven.
Straight-wall charger housings molded without slides: 163 mm tall, VDI 30 texture, no drag marks on the side walls.
Cavity-core pull and a mother-cavity ejection layout remove the thick-to-thin flow mark that shows as a bright edge on PC housings.
Two- and four-side slide tools with calculated thermal growth of slide and cavity, so batch after batch the parting line stays below hand-feel.
How a project runs
A fixed sequence, with documented checks between each step.
We review the 3D model, wall thickness, gate position and texture, then quote tooling and part price.
Cavity layout, cooling, ejection and slide design are agreed before machining starts.
Machining, fitting and T0 trial. First articles are measured and sent for approval.
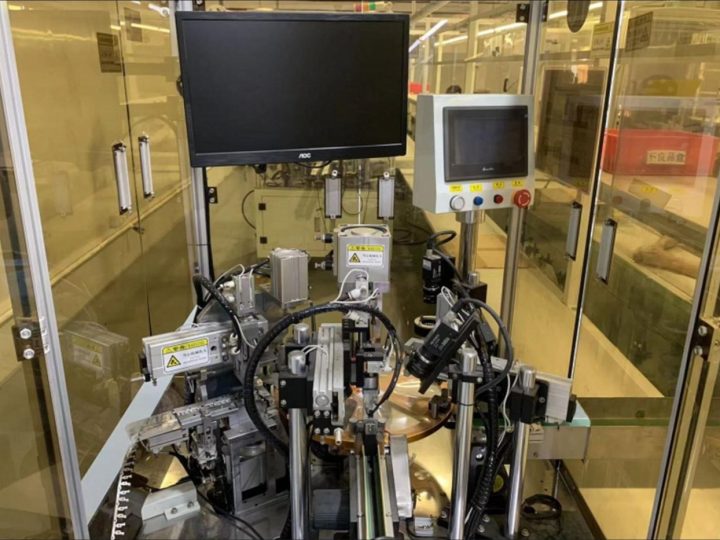
Molding, in-line inspection and automatic secondary operations run to the approved parameters.
Final inspection, RoHS documentation where required, packing and shipment.
Quality & laboratory
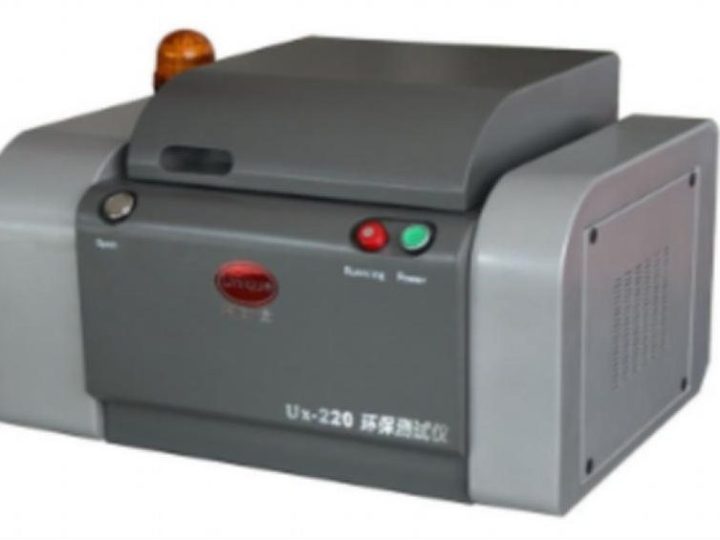
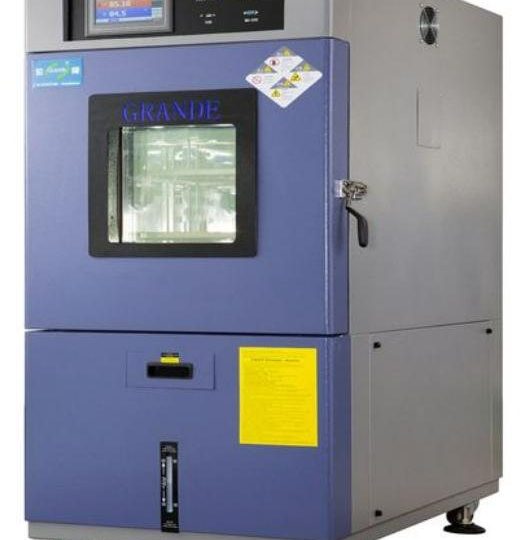
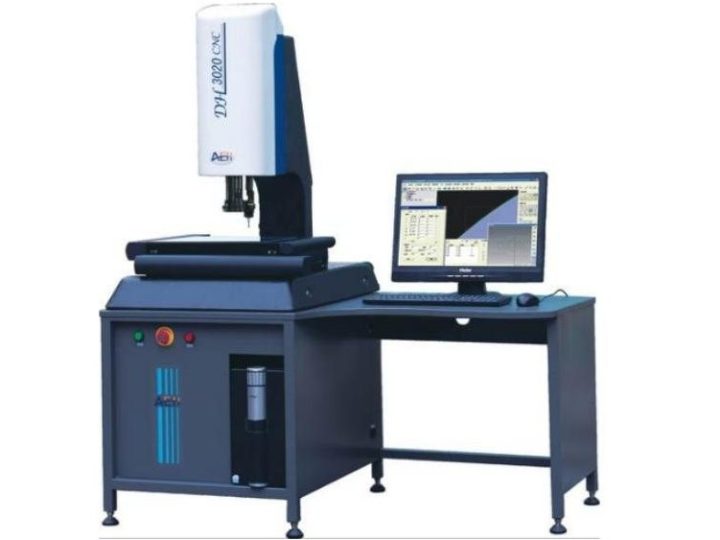
Incoming resin, in-process parts and outgoing shipments are inspected by a 15-person quality team, using RoHS screening, salt spray, melt flow index, color and gloss measurement, drop and ball-impact tests, and a high-low temperature chamber.
Certification
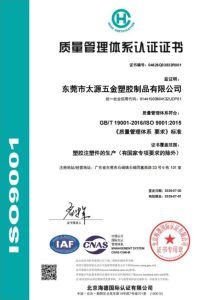
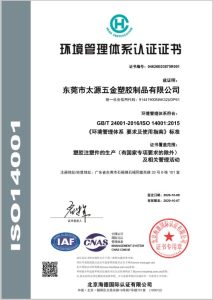
The quality and environmental management systems are certified by a third-party body. Certificates are available for download and can be sent with your quotation package.
View certificatesEngineering notes
Three secondary operations decide whether a housing is reliable: trimming the gate, inserting the pins and riveting the spring contacts. Here is…
Read the noteOn a tall housing with side openings, the slide and the cavity run at different temperatures. Calculating the thermal growth of both…
Read the noteA straight housing wall has no draft to help it leave the tool. Here is how we mold a 163 mm tall,…
Read the noteTell us the part, the housing style, the annual volume and the market. We will reply with a feasibility note, tooling approach and lead time.